How to Choose the Right Reamer Drill Bit?
Choosing the right Reamer Drill Bit is not a catalog exercise. It is a decision about formation, hole size, drilling method, and the equipment already on site. A bit that cuts cleanly in soft ground may chatter, wear unevenly, or slow progress in abrasive rock. Small details matter: a worn gauge, an unsuitable cutter layout, or poor fluid clearance can change the feel of the whole drilling run.
Industry reports help set the context, but they have limits. The U.S. Geological Survey’s Mineral Commodity Summaries and the World Mining Data report track mineral production and related industry trends; neither should be treated as a direct measure of reamer-bit performance. For selection, compare the manufacturer’s technical specifications with the actual formation, required diameter, connection, and operating conditions. Check cutter material, body design, and compatibility with the drilling assembly. Ask for documented wear or field-performance data when available. Then verify the choice against the site’s own drilling records. A tidy specification sheet is not field proof.
One point deserves care. No source material or independently verifiable quotation from a named Reamer Drill Bit specialist was supplied, so I will not invent one. That omission is intentional. The practical lesson remains: match the tool to the ground, and treat assumptions as assumptions. A short trial can reveal what a brochure cannot. Real conditions decide.
Understand the Purpose and Function of a Reamer Drill Bit
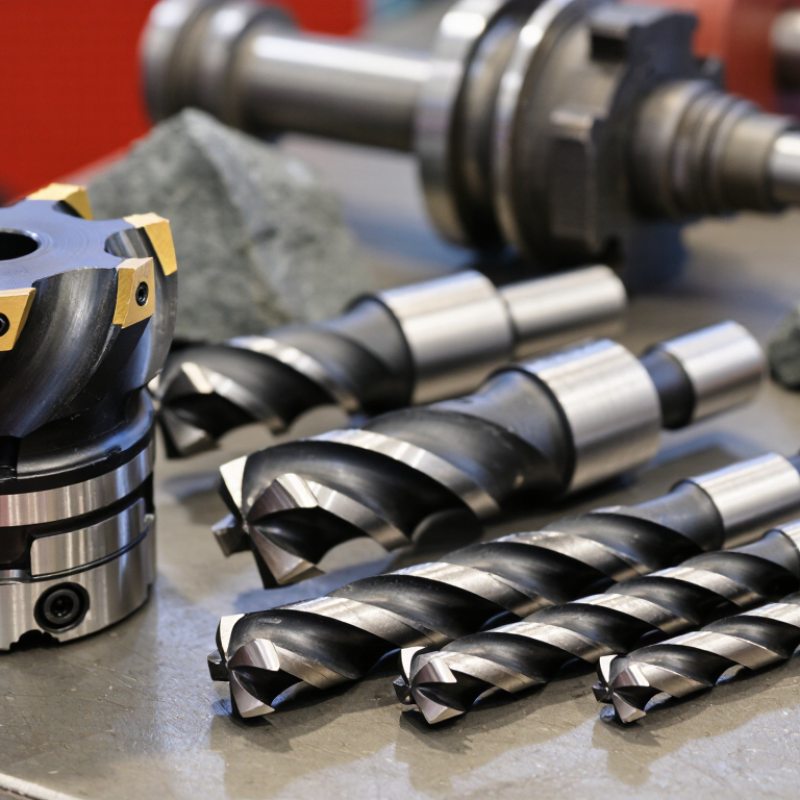
A reamer drill bit refines an existing hole. Its cutting edges remove a small amount of material, helping bring the hole closer to a chosen diameter and improve its finish. It is not designed to make a fresh hole from solid stock. Not for starting holes.
The pilot hole matters. If it is too small, the reamer may remove too much material, bind, or wear unevenly. If it is too large, the finished hole may not have enough material left for accurate sizing. Check the tool’s specifications and the workpiece material before use. A light coating of suitable cutting fluid can help reduce friction and carry chips away.
It is tempting to treat a reamer as a quick fix for a rough hole, but that can produce uneven results. Keep the tool aligned with the hole and use a controlled, steady feed; forcing it can damage the cutting edges or the workpiece. Cutting speed varies with tool material, workpiece, and setup, so follow reliable machining guidance rather than guessing. Even careful work may need a final measurement with an appropriate gauge.
Identify the Material and Hole Requirements
Start with the workpiece, not the tool catalog. Aluminum cuts easily, but it can smear and cling to cutting edges. A sharp reamer and suitable cutting fluid help limit built-up material. Stainless steel creates more heat and may work-harden if the tool rubs instead of cutting. Cast iron is abrasive, so edge wear deserves attention. Material labels can mislead; an alloy’s condition also changes how it cuts. Check the workpiece specification when the exact material is uncertain.
Then define the hole. Note its finished diameter, tolerance, depth, and whether it passes through the part. A blind hole needs room for the reamer’s lead and chips; otherwise, the tool may bottom out or leave a rough end. Keep the pilot hole straight and close to the required size, while following the reamer maker’s recommended stock allowance. Too much material can overload the edges; too little may make the tool rub. And yes, a careful setup can still leave a bell-mouthed hole. A test cut in scrap can reveal alignment or finish problems before the actual part is machined.
Choose the Right Reamer Type, Size, and Geometry
How to Choose the Right Reamer Drill Bit?
Choose the Right Reamer Type, Size, and Geometry
Match the reamer type to the hole and the machine. A straight-flute reamer suits many general-purpose jobs, while a spiral-flute design can help clear chips from blind holes. For through-holes, chip direction and workpiece material still matter. Check the tool’s specifications rather than assuming one flute style works everywhere. A reamer removes a small amount of material; it is not meant to correct a badly misplaced or undersized hole.
Tips: Measure the drilled hole and the required finished diameter. Leave the recommended reaming allowance for your material and tool. Too little may cause rubbing; too much can produce chatter or a rough bore. Small details matter.
Choose a reamer size based on the final hole diameter, then confirm the tolerance and measurement method. Geometry matters, too. A short lead chamfer can guide entry, while flute count and helix affect chip flow and finish. Use a stable setup, align the tool with the hole, and apply suitable cutting fluid when the material calls for it. I would not rely on appearance alone: even a clean-looking hole can be slightly out of round. Check a sample with an appropriate gauge before running a full batch.
Check Tool Compatibility and Operating Conditions
Choose a reamer only after checking the machine, holder, and hole material. Match the shank to the holder, and confirm the tool’s diameter and reach suit the setup. A long overhang can amplify vibration. Check spindle runout at the holder, not only at the spindle nose. Small errors matter.
Set speed and feed for the reamer material, workpiece, and coolant conditions. Use the toolmaker’s recommended cutting data when available, then adjust cautiously if the setup differs. Clear chips from blind holes; trapped chips can score the finished bore. Keep coolant directed into the cutting zone. It is easy to overlook.
Set a realistic size target before choosing the tool. ISO 286-1:2010 lists an IT7 tolerance of about 18 μm for nominal diameters from 10 to 18 mm. That figure describes the workpiece tolerance band, not a guarantee of reamer performance. Machine condition, runout, stock allowance, and material can all affect the result. I would verify the actual hole with a calibrated gauge after a trial cut; the first pass may reveal a setup problem, not a bad tool.
How to Choose the Right Reamer Drill Bit? Check Tool Compatibility and Operating Conditions
Typical starting cutting-speed ranges for high-speed steel (HSS) reaming are shown in metres per minute. Actual recommendations depend on the reamer material and geometry, workpiece grade, hole depth, coolant, and machine rigidity—check the tool maker’s guidance. To estimate spindle speed, use RPM = (cutting speed × 1000) ÷ (π × reamer diameter in mm). Confirm shank and diameter compatibility, use a suitable lubricant, and feed steadily without stopping in the hole.